Skip to content
AFArcFort Weld
Menu
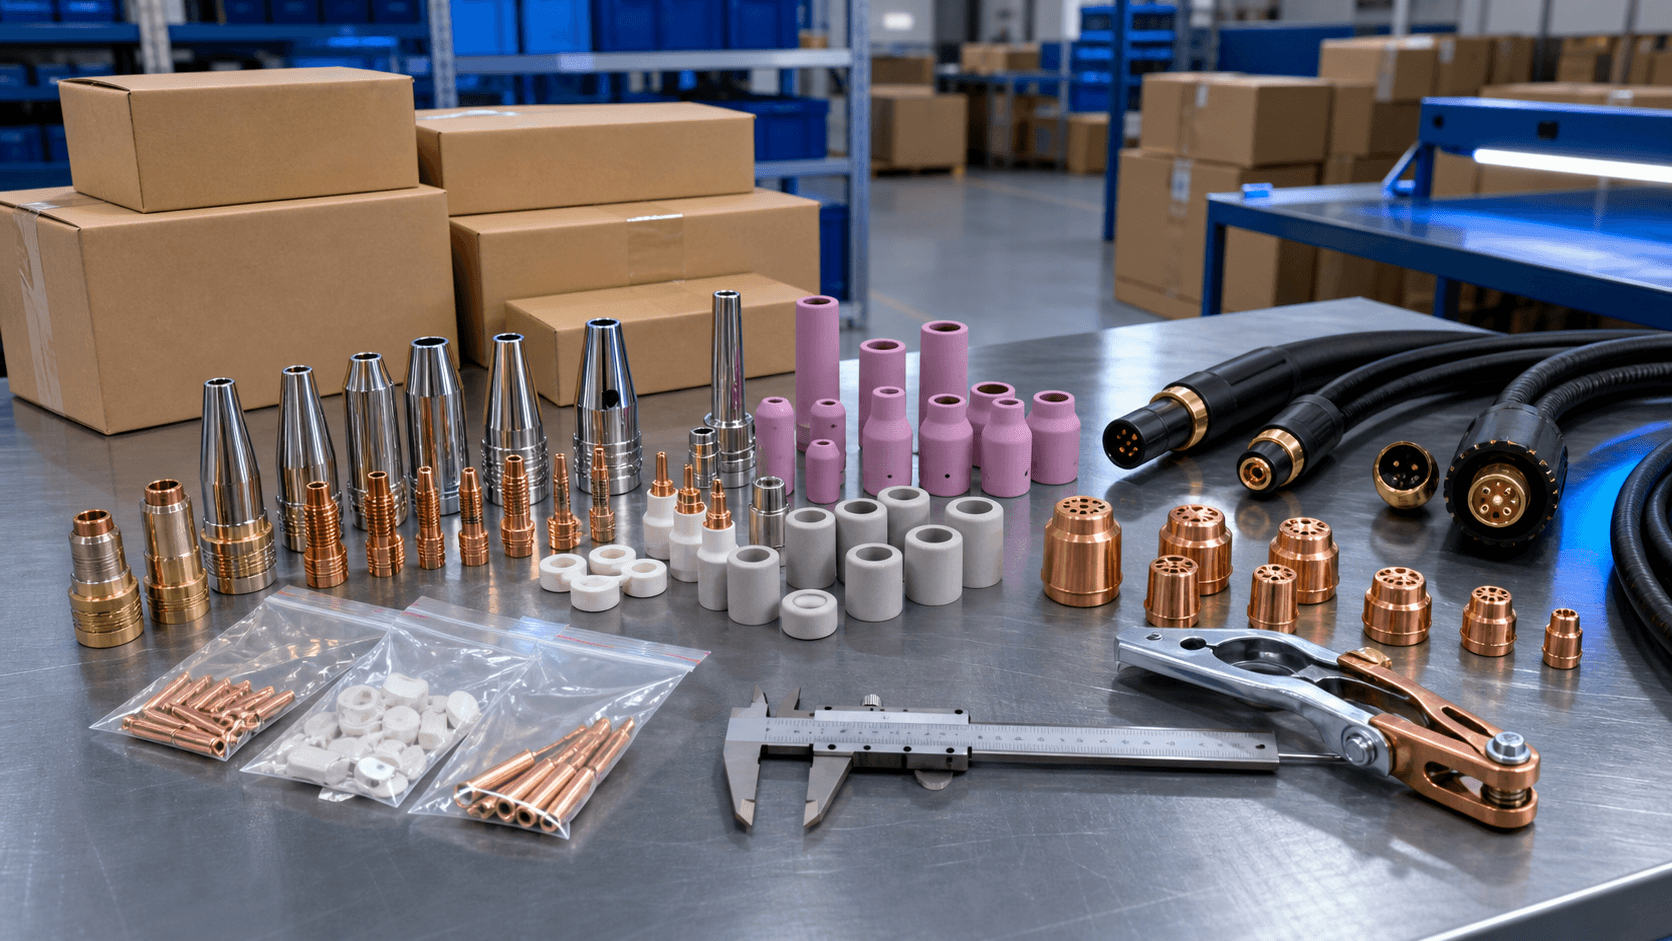
Representative welding products arranged for reference and packing review

Order-Specific Quality Coordination

Quality control starts with an approved product reference.

Define the item, compatibility basis, critical details, packing and required evidence before production planning and shipment approval.

The inspection scope varies by product and order. Requested photos, measurements, samples or records must be confirmed in the quotation or approved order details.

Representative product-review image; inspection scope is confirmed by order

Inspection Workflow

Four approval points tied to the order record.

Buyer evidence defines what can be reviewed, when approval is required and which record should be retained for the quoted item.

  1. 01

    Product reference review

    Buyer evidence

    Itemized RFQ, existing part number, torch or machine label, drawing, measured details, product photos or a physical sample.

    Review focus

    Separate confirmed product identity from open material, dimension, thread, rating and compatibility fields before quotation approval.

    Order record

    Quoted item reference, buyer-supplied evidence and any technical details still requiring approval.

  2. 02

    Pre-production readiness

    Buyer evidence

    Approved product reference, quantity by line, packaging requirement, artwork version and any requested inspection evidence.

    Review focus

    Check that the product, customization and packing basis is sufficiently defined before production planning or order preparation.

    Order record

    Approved order details, open actions and the inspection or sample-approval scope agreed for the order.

  3. 03

    Product and first-piece review

    Buyer evidence

    Critical dimensions, appearance points, interface details or approved sample criteria that matter to product selection and fit.

    Review focus

    Review applicable dimensions, thread, profile, finish, assembly or identification against the agreed reference. Methods vary by product.

    Order record

    Measurement, photo or sample evidence when requested and confirmed as part of the quotation or order.

  4. 04

    Packing and pre-shipment review

    Buyer evidence

    Packing unit, labels, barcodes, carton marks, destination requirements and the final approved item list.

    Review focus

    Reconcile product identity, quantity, packing presentation, marks and requested shipment documents before dispatch approval.

    Order record

    Final packing basis, shipment-document scope and pre-shipment evidence agreed for the order.

Product Review Matrix

Different product families fail for different reasons.

This matrix prepares the evidence needed to distinguish the requested item. It does not treat a broad model name or similar appearance as confirmed compatibility.

01

MIG/MAG torch parts

Common mismatch risk

Similar-looking contact tips, tip holders, diffusers, nozzles and liners can differ by thread, bore, length, profile or torch series.

Buyer should send

Torch label, current consumable photos, wire size, measured thread and key dimensions, plus any reliable part reference.

Lock before order

Part type, thread, wire or bore size, profile, key dimensions, torch reference and packing unit.

02

TIG torch parts

Common mismatch risk

Ceramic cup number, collet size, collet-body or gas-lens thread and torch-family references are not interchangeable by appearance alone.

Buyer should send

Torch model or label, electrode diameter, current consumable stack photos, thread details and sample or drawing when available.

Lock before order

Cup size, electrode size, thread or interface, torch reference, component type and packing unit.

03

Plasma cutting consumables

Common mismatch risk

Electrodes, nozzles, shields and swirl rings must match the torch system and the correct position in the consumable stack.

Buyer should send

Torch or system label, full consumable-stack photos, existing reference numbers and measured details or samples.

Lock before order

Torch reference, component position, nozzle orifice when documented, profile, key dimensions and complete item list.

04

Welding consumables

Common mismatch risk

Consumable type, nominal size, material requirement, packaging format and destination documentation can change the correct item.

Buyer should send

Current label or data sheet, required type and size, material requirement, quantity, packing and destination country.

Lock before order

Product type, supported material and size data, packing, quantity and available document scope.

05

Welding and cutting machines

Common mismatch risk

Process, input supply, output requirement, duty expectation, connector type and included accessories must be reviewed together.

Buyer should send

Required process, input voltage and frequency, target output range, workpiece context, connector preference and destination requirements.

Lock before order

Quoted model, documented ratings, included accessories, plug or connector requirement, packing and document scope.

06

Welding accessories

Common mismatch risk

Cable connectors, holders, clamps and related accessories can differ by connection standard, cable range, contact interface and assembly.

Buyer should send

Current item photos, connector or interface details, cable requirement, measured dimensions, quantity and intended application.

Lock before order

Accessory type, interface, supported size or cable range, assembly scope, quantity and packing unit.

Buyer and Supplier Controls

Compare each requirement with a written confirmation.

Unknown values stay open until they can be traced to a drawing, sample, label, measurement or reviewed document.

Product identity

Buyer input

One line per item with product name, model or reference, quantity and a photo, drawing or sample reference where fit matters.

Supplier confirmation

The exact quoted item and included components, with similar-looking alternatives kept on separate lines.

Technical fields

Buyer input

Critical size, thread, material, rating or interface requirements, identifying which values are measured and which are expected.

Supplier confirmation

Only supported values, the evidence basis and a clear list of details that remain available upon request or require a sample.

Compatibility

Buyer input

Torch or machine label, complete component stack, existing reference and the dimensions needed to distinguish the part.

Supplier confirmation

Whether fit is confirmed, reference-only or still unverified. A family name alone is not treated as confirmed fitment.

Packing and identification

Buyer input

Unit quantity, inner packing, label, barcode, logo, carton artwork and shipping-mark requirements.

Supplier confirmation

Approved packing unit, artwork version, carton basis, customization scope and related MOQ or schedule effect.

Inspection evidence

Buyer input

The required photo, measurement, sample, packing or pre-shipment record and when approval is needed.

Supplier confirmation

Available evidence, review method, timing and any cost or lead-time effect stated before the order is approved.

Evidence Options

Ask for the required record before order approval.

Availability, format, timing and cost vary by SKU and order. State the requirement in the RFQ so it can be confirmed in writing.

Reference sample or drawing
Use an approved sample, marked drawing or dimensional reference when a product name or photo cannot establish exact fit.
Product and measurement photos
Request the required views and measurement points during the RFQ stage. Availability and scope are confirmed for the specific order.
Packing artwork and marks
Approve the label, barcode, inner-pack quantity, carton artwork and shipping marks before customized packing is prepared.
Pre-shipment record
Define the item, quantity, packing and document evidence needed before balance payment or dispatch approval.

Certification and Compliance Requests

Certification is not assumed from a product family or similar model. State the destination market, exact product and required document during quotation. ArcFort Weld will confirm only the documents available for the specific quoted item.

Quality Coordination FAQ

What quality information should a buyer send with an RFQ?

Send an itemized product list, model or existing reference, quantity and the technical details that affect fit. Add clear photos, labels, drawings, measured dimensions or sample information when the part is not fully identified.

How is welding torch or plasma consumable compatibility reviewed?

Compatibility is reviewed from the torch or machine model, existing part reference, complete consumable stack, measured details, drawing or physical sample. A similar appearance or broad family name is not sufficient to confirm exact fit.

Can buyers request inspection photos or measurement records?

Yes. State the required views, dimensions, quantity of samples and approval timing in the RFQ. ArcFort Weld will confirm which records are available and include the agreed scope in the quotation or order details.

Can a sample be approved before a regular order?

A sample or pre-production approval can be discussed when product identification, fit, appearance or customized packing requires it. Sample availability, cost, dispatch method and approval effect on lead time are order-specific.

How are private-label packaging details controlled?

The buyer should approve the logo, label content, barcode, packing unit, carton artwork and shipping marks. The quotation should identify the approved version and any customization-related MOQ or lead-time requirement.

Does ArcFort Weld claim certifications for every product?

No. Certification and destination-market document requirements must be stated by product and order. Documents are only confirmed when they are available for the specific quoted item.

Request for Quotation

Define the inspection scope with the product RFQ.

Send the itemized list, model or current reference, critical details, quantity, compatibility evidence, packing requirement and the inspection records you need.